Commercial HubHyderabad, Telangana
Corporate Headquarters — Hyderabad
Our headquarters in Hyderabad houses corporate leadership, strategic raw material procurement and regulatory documentation services.
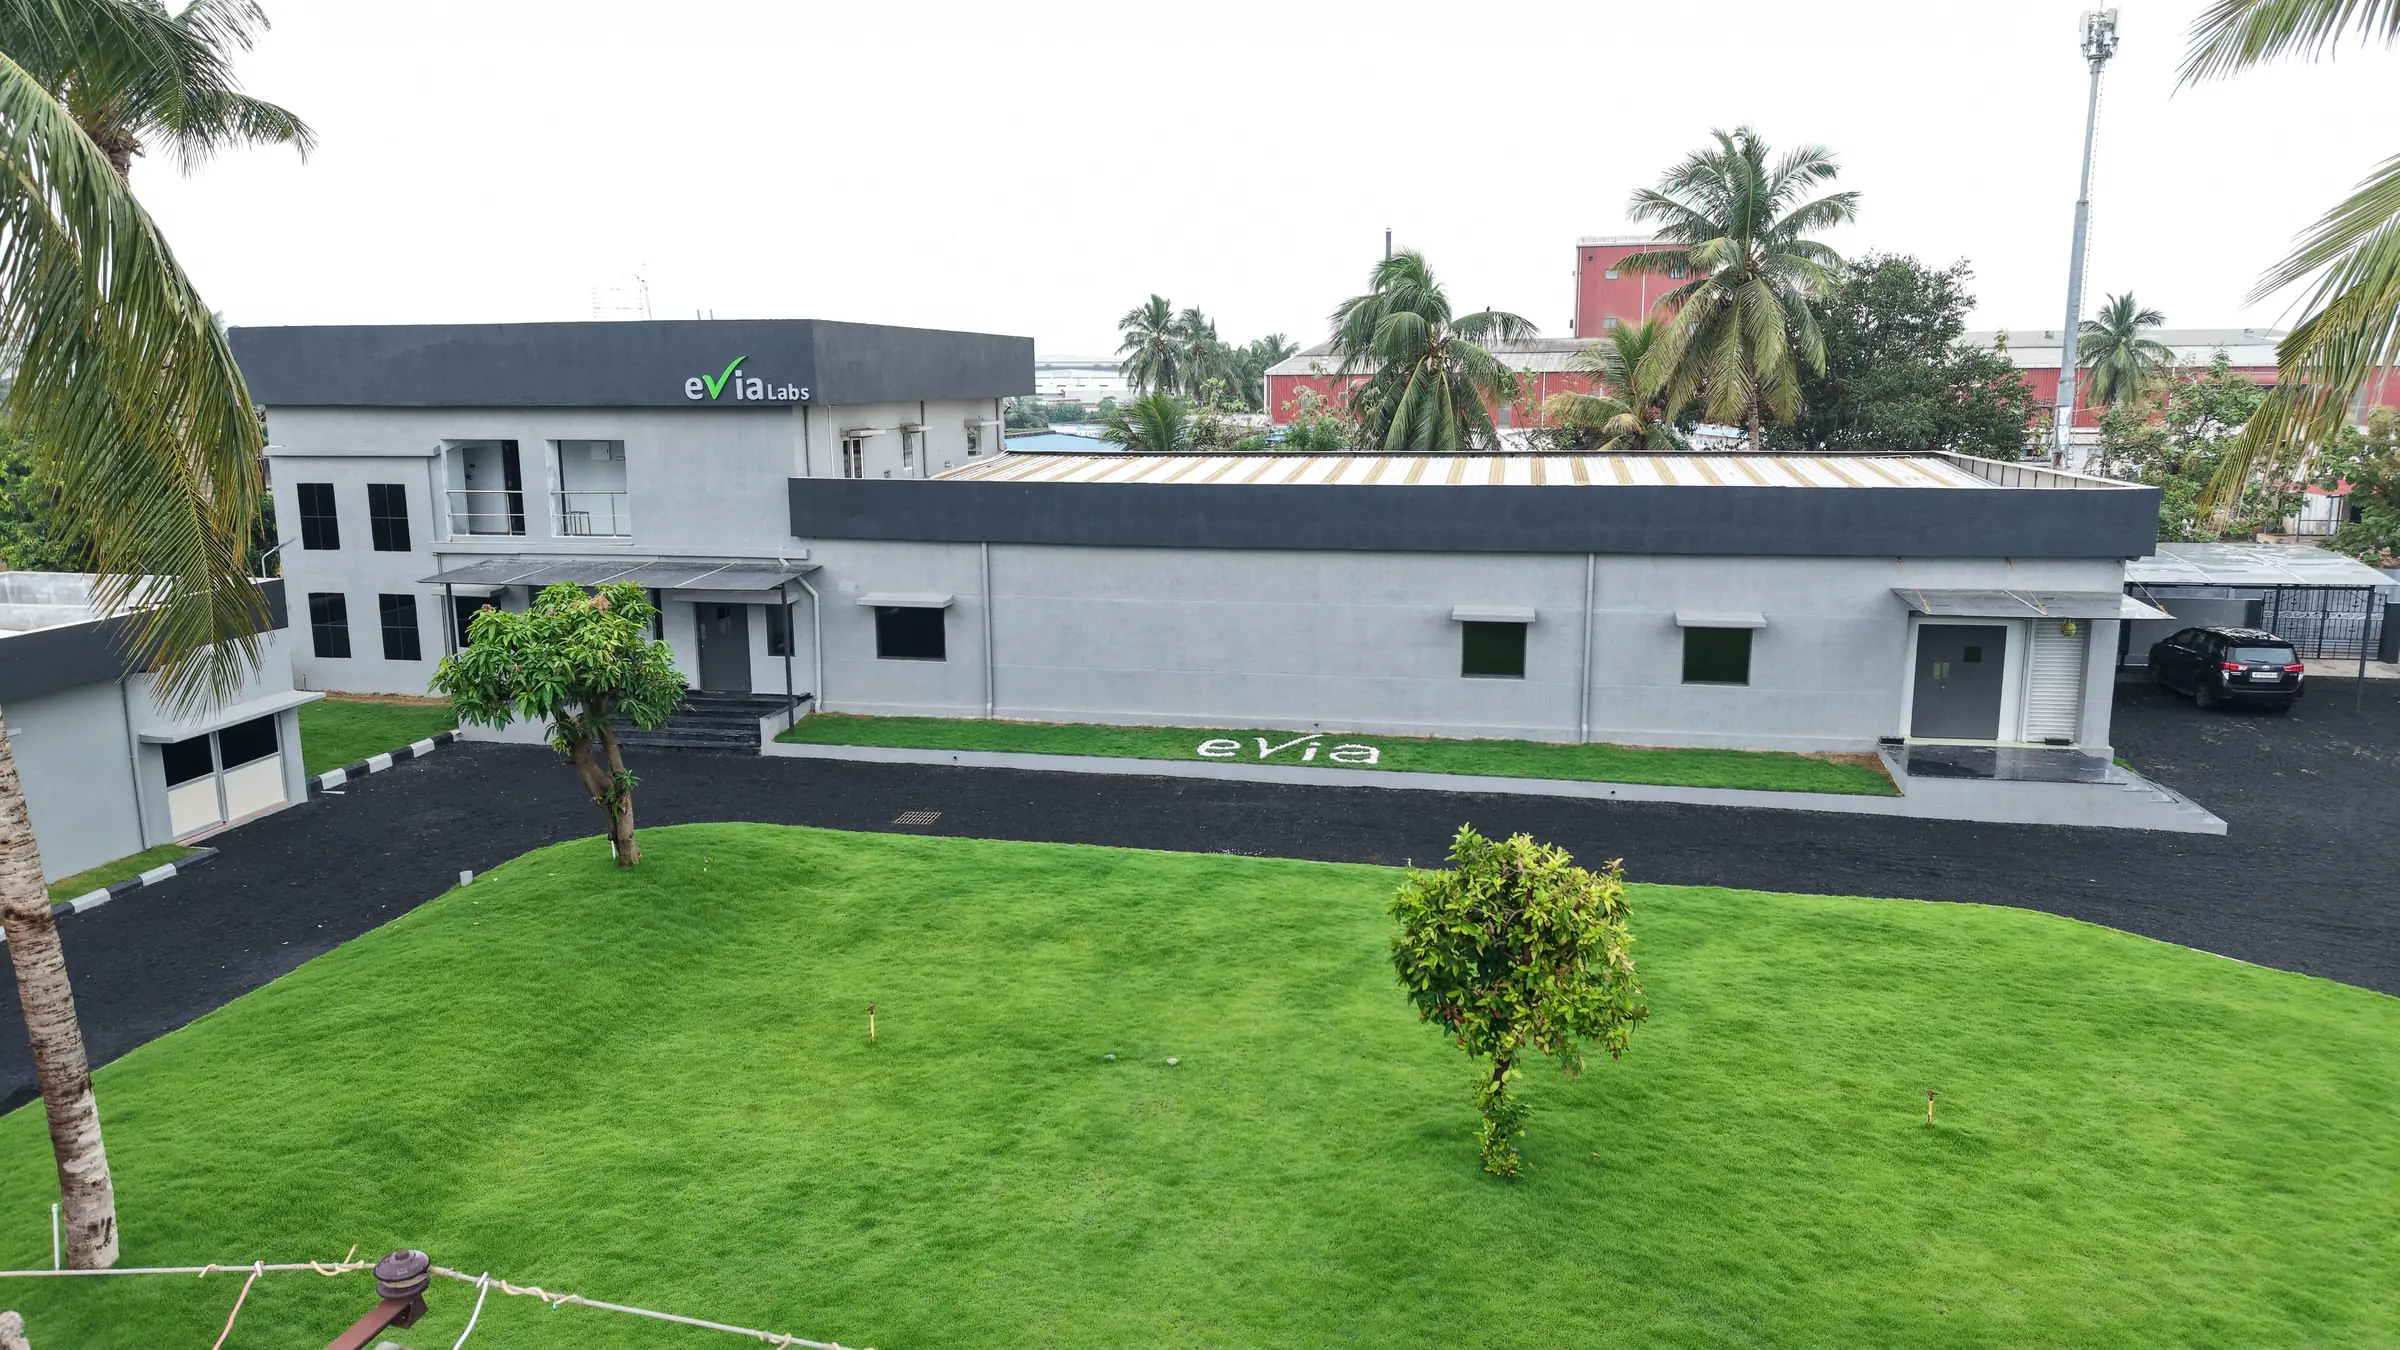
Founded on the belief that nutritional formulations warrant the unyielding scrutiny of therapeutic drugs, eVia Labs bridges the gap between laboratory science and scalable industrial delivery. Rooted in Hyderabad and powered by our manufacturing campus in Andhra Pradesh, we deliver validated potency, zero-compromise purity, and uncompromising repeatability to modern wellness brands worldwide.
When we founded eVia Labs, I wanted to bring the discipline I valued in pharmaceutical manufacturing to nutraceuticals. A promising formulation is only the beginning. We also have to understand how to manufacture it consistently and how it holds up over its intended shelf life.
At our facility, we work with wellness and pharmaceutical partners in India and abroad. Whether we’re developing a new formulation or transferring one a partner already trusts, we agree on the specifications early and carry them through to commercial production.
When a partner puts their name on a product we make, they’re trusting us with their reputation. I want them to know how their product was made, how its quality was checked, and what they can expect when they place their next order.
Our organizational model distinctly separates commercial and regulatory leadership from scalable industrial production, ensuring operational excellence across every engagement.
Our headquarters in Hyderabad houses corporate leadership, strategic raw material procurement and regulatory documentation services.
Our state-of-the-art solid dosage manufacturing facility in Andhra Pradesh is purpose-built for cleanroom production, controlled tablet compression, encapsulation, and finished packaging.
The foundational manufacturing principles that govern our operations and product integrity.
Strict cleanroom modular design with positive-pressure HEPA filtration, strict environmental temperature and humidity parameters, and continuous cross-contamination barriers.
Rigorous procedural discipline and batch record verification ensuring uniform active compound distribution and identical dissolution parameters across every production run.
Exhaustive raw material testing, verified Certificates of Analysis (CoA), and comprehensive documentation designed to satisfy domestic and international regulatory reviews.
From pharmaceutical organizations establishing preventative health divisions to fast-scaling wellness brands and international distributors.
Expanding into preventative healthcare and therapeutic food formats without risking corporate brand equity or regulatory deviation.
Requiring dependable batch reliability, consistent taste and texture, low variation, and rapid turnkey packaging adaptation.
Making products that meet international quality standards, with the documentation needed to register and sell them in overseas markets.
Connect with our technical and regulatory teams to evaluate formulation feasibility, packaging specifications, and commercial manufacturing timelines.